-

Small busbar production process
Learn how copper busbars are manufactured, from raw material selection to cutting, stamping, CNC machining, plating, and final inspection for electrical and grounding systems. Whether you're planning a production line, optimizing your current setup, or simply understanding the busbar fabrication process. This article explains how copper busbars are manufactured in the UK. It gives a thorough explanation of the steps taken to turn raw copper into a finished conductor. This article will walk you through each critical stage of producing a bespoke copper bus bar, emphasizing the. Busbar manufacturing is the process of fabricating conductive strips, typically made from copper or aluminum, to distribute electricity efficiently in electrical busbar systems. These conductors are found in switchgear, control panels, busbar trunking, and high-capacity power distribution units. The process of busbar manufacturing involves cutting, bending, and drilling these metals into specific shapes and sizes to meet the precise requirements of various applications. Their design significantly reduces the space.
[PDF Version]
-
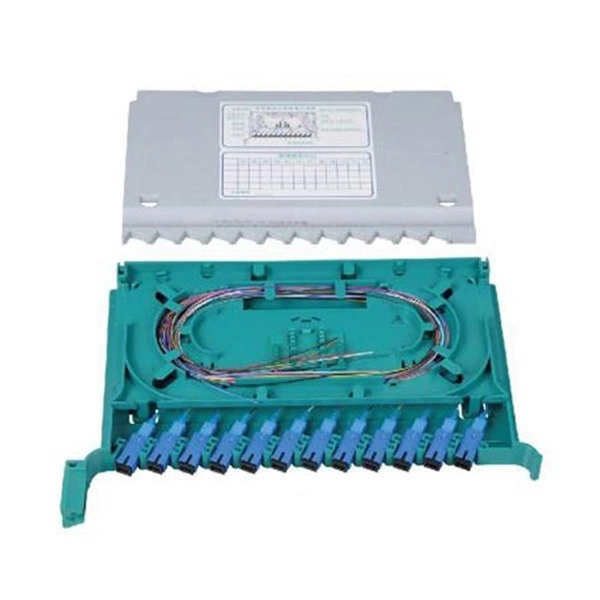
What are the main components of the optical module TX manufacturing process
Three main components make up the optical module: the external visible housing, the optoelectronic components, and the PCBA. Among them, transceiver design is the basis for optical transceiver production. It involves many fields such as optoelectronics and circuit design to ensure the performance and stability of. In the era of 5G, AI, and high-speed data centers, optical modules serve as the core bridge for converting electrical signals to optical signals (and vice versa), enabling fast, reliable data transmission across networks.
-
Cold Joint Manufacturing Process Flow
Cold working is the process of metal forming in which the deformation of metal occurs below its recrystallization temperature. In most cases, We perform cold working of metal at room temperature. You migh.
-

Customization Process for Low-Noise Fiber Bragg Gratings for Backbone Networks
Figure 1 illustrates the proposed reconfigurable grating. The grating consists of multiple series-connected uniform Bragg grating sections and a Fabry-Perot (FP) cavity section in the center of the grating. Each u.
-
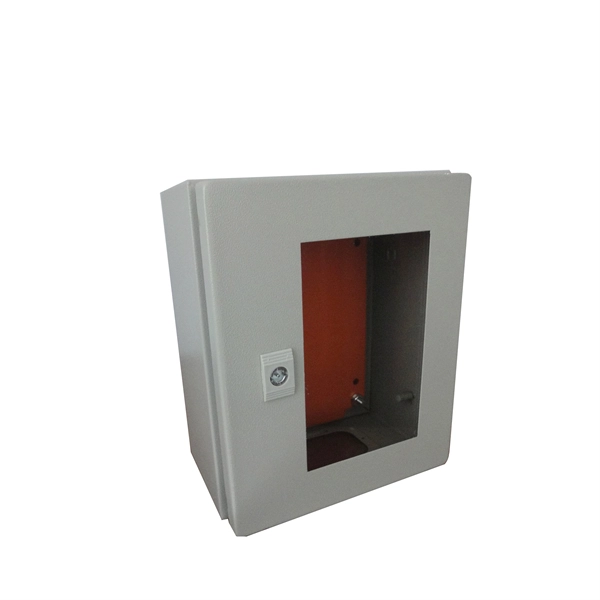
Wiring process for relay protection panels
This handbook covers the code of practice in protection circuitry including standard lead and device numbers, mode of connections at terminal strips, colour codes in multicore cables, dos and donts in execution. presentation of protection and control relaying. It covers standard codes, wiring practices, and norms for protecting generators, transformers, and lines, and provides detailed. Document converted into new template and updated throughout to reflect details of protection panels, relays and schemes currently in use. The copyright of this document, which contains information of a proprietary nature, is vested in Electricity North West Limited. The HT power supply is received from GO switch and distributed to the.
-

British Fiber Bragg Grating Strain Measurement Process
The purpose of this paper is to introduce a method for direct measurement of dynamic stresses in optical fiber during processing, deployment, and in-service lifetime. This method employs the well known strain dependence of fiber Bragg gratings. Fiber Bragg gratings have been used to measure. The work is devoted to the consideration of methods for determining the strain of objects using fiber Bragg gratings under a high-frequency vibration or pulsed mechanical action, which is difficult to perform using widespread methods and devices. The methods are based on numerical processing of the. Fiber Bragg Grating Sensors (FBGS) are gaining increasing attention in the field of experimental stress analysis.
-

Installation process of optical fiber cable in ducts
Installing duct fiber requires specialized techniques to navigate ducts (which may have bends, joints, or obstacles). The two most common methods are pulling and air blowing —each with unique advantages and use cases. The pulling method uses mechanical force to pull the cable. Corning Optical Communications cable specification sheets are available which list the maximum tensile load for various cable types. The installation process is influenced by local conditions, local climate, customer's existing procedures, and customer requirements. ulling has been the first technology for installing OF cables in duct. It. Where reels are supplied with protective material fitted over the cable, the protection should remain in place until the cable will be installed. The cable should be bent as little as possible.
[PDF Version]
-
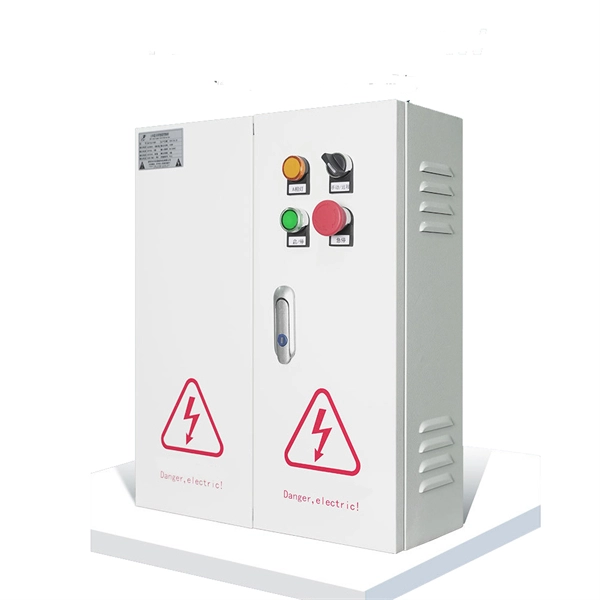
Connection process between butterfly-shaped optical cable and prefabricated terminal
Fusion splicing is a popular method of connecting butterfly-shaped optical fiber cables. The two fiber cables are stripped of their protective coatings, and their bare ends are aligned and then fused together using a fusion. The utility model belongs to the technical field of communication equipment, in particular to a prefabricated end butterfly-shaped optical cable connector, which comprises an inner sheath, one end of the inner sheath is sleeved with an outer sheath in a sliding way, a sliding groove corresponding. Butterfly-shaped optical fiber cables are a popular type of fiber optic cable that is commonly used for data transmission in telecommunication networks. This design allows for easy installation and termination, as multiple fibers can be spliced or connected at once. In this. FTTH Butterfly Optic Cables are specifically designed to meet the growing demand for high-speed fiber-to-the-home deployments. The intraductal through -hole that is equipped with of backstop.
[PDF Version]
-

Standard manufacturing length of optical cable
Standard/default length is 2 inches (reference), as produced by most label manufacturers. Marking details are based on MIL-STD-130 and will be legible and permanent. Cage code = 0YPM2 for AFSI, part number = 2006112209MD-01, serial number with. ITU-T has been active in the standardization of optical communications technology and the techniques for its optimal application within networks from the infancy of this industry. Fiber optic networks rely on a foundation of rigorous international standards that define. Bundles up to 3925FT in length (1. 87 in active diameters you specify. Fiberoptics Technology also supplies fused doped silica fiber with an NA of. 5 Sample length: Not less than 50m. This work materialized through the development of good practices, procedures and specifications documents, reflecting a certain state of the art at a given time, and the result of a consensus of all stakeholders (op lable.
[PDF Version]
-
Electrical Distribution Box Cover Manufacturing Scheme
This guide will help you understand the electrical enclosure manufacturing process, thus ensure you have a successful purchasing experience. Let's dive right in.