-
How much does fiber distribution box welding cost per core
For most commercial projects, expect to pay $50–$150 per fusion splice point - but that number can swing in either direction based on the factors below. This refers to the cost of electrical power used for welding. Direct labor cost of welding usually covers the wages of the welder and the helper who helps. I usually bill T&M, but it works out to about $175-250 for setup/teardown per site and $4-7 per fiber for prep in a new tray in an existing case and splicing depending on if it's flooded or dry cable. Add another $50-75 to prep a new case endspan or $100-150 for a new case midspan with overcut on. Fiber optic splicing costs vary widely depending on project size, location, fiber type, and site conditions. The "per splice" rate is the most. The fiber splitter distribution box supports fiber splicing, splitting, distribution, "three in one" and fiber optic distribution box also offers solid protection and fiber cable management for FTTX network installation. Whether for indoor FTTH terminal points or rugged outdoor distribution nodes, OTRANS has.
[PDF Version]
-
What are some photovoltaic module products
There are four main types of solar panels: monocrystalline, polycrystalline, thin-film, passive emitter, and rear cell (PERC) solar panels. A solar module, also commonly referred to as a solar panel, is a packaged assembly of photovoltaic cells that converts sunlight directly into electricity through the photovoltaic effect. First invented by Charles Fritts in 1883, the solar panel has undergone an evolution in the last 200 years, leading to a diversification of the PV materials used. This report, drawing on the latest developments in the 2025 market, analyzes the key characteristics of the top 10 global PV module manufacturers across four dimensions: technological capability, vertical integration, international presence, and performance in the European market. They utilize the photovoltaic effect, a scientific principle where.
[PDF Version]
-
Corresponding ferrules for different fiber optic patch cords
☆ The SC connectors for SC-SC fiber patch cords are of push pull design, being fit for 3. At ZION Communication, we design and manufacture a full range of fiber patch cords for: This guide will help you quickly understand the main types of. The ferrule end face of the patch cord is ground into different structures. PC, APC, and UPC are three different ferrule polishing methods, representing the structural differences of the front face of the ceramic ferrule. Ceramic ferrules are well known for having high durability and the highest levels of dimensional control, making them suitable for use. The most obvious method was to use a machined V-groove as an alignment tool and to secure the two fiber ends within metal tubes or ferrules in such a way as to ensure acceptable performance.
[PDF Version]
-

Transceiver and Optical Module Pairing
This guide dives deep into the core aspects of optical transceiver compatibility, common interoperability challenges, and practical strategies for network engineers, IT managers, and purchasing professionals aiming to deploy reliable, high-efficiency optical links. This section describes how to install optical transceivers on the SFP or SFP+ ports and connect them to the ports of the peer device using optical fibers according to the network plan. The USG supports both 1 Gbit/s, 10 Gbit/s, and 40 Gbit/s optical modules. The optical modules at both ends are. How to Ensure Interoperability Between Two Optical Transceivers? When it comes to the connection between two fiber optic transceivers, the following four factors should be taken into considerations: wavelength, speed, fiber type, and the connection to switches. In a fiber link, the data is. Integrated circuits and reference designs help you create a smaller and faster optical module design used in high-bandwidth data communication applications.
[PDF Version]
-
Pairing at both ends of the optical module
Type A (Straight-Through): Fiber sequence 1–12 matches at both ends. Ideal for direct optical module-to-module connections. Polarity in fiber optic networks refers to the alignment of transmit (Tx) and receive (Rx) signals between interconnected devices. However, the following conditions must be met for this configuration to work: 1. Speed negotiation – The SFP+ module needs to be dual-rate to operate at the same speed as the SFP. This section describes how to install optical transceivers on the SFP or SFP+ ports and connect them to the ports of the peer device using optical fibers according to the network plan. The optical modules at both ends are. MTP/MPO with 8 or 12 fibers is typically used in data centers to connect fiber distribution frames in duplex applications or end-to-end parallel fiber applications (such as 40, 100, 200, and 400Gbps) that use 8 fibers for transmission and reception (4 at 25, 50, or 100Gb/s, and 4 at 100Gb/s).
[PDF Version]
-
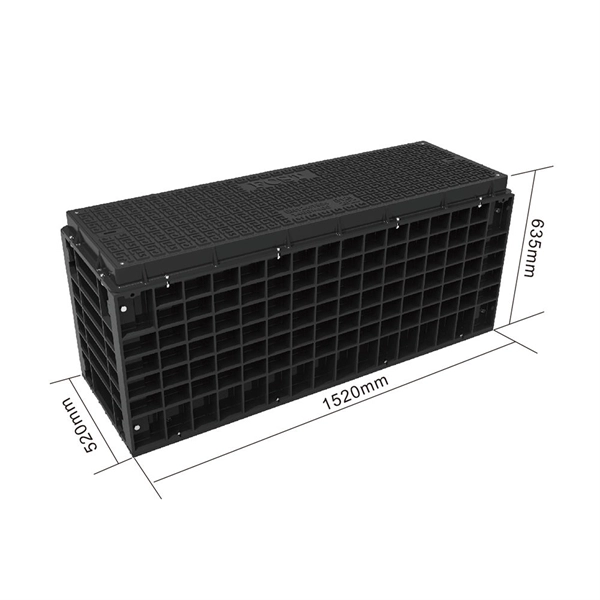
Does the welding machine need to be grounded when connected to the distribution box
The machine is automatically grounded when it is plugged into the power. For this reason, you should never remove that pin or use any type of adapter with these welding machines. Applying and maintaining proper grounding methods within the welding area is important to promote electrical safety in the workplace. Associated processes such as plasma cutting will also benefit from proper grounding. Without it, you can have a weak weld, a. One of the first things that any new welder learns is that whatever they're welding, it should be grounded, and if you don't have it grounded correctly, then your welding quality, your consumables, and your equipment will suffer in the long run. Ensure a secure connection and avoid thin or sharp edges, which can cause resistance, overheating, or arc instability.
[PDF Version]
-
Metal welding of distribution boxes
In the manufacturing process of metal distribution boxes, welding constitutes a critical stage following sheet metal cutting and bending. Ever wondered how the sturdy distribution boxes controlling electricity in buildings, factories, or even outdoor solar installations hold their shape so reliably? The answer lies beneath the surface - in the powerful art of welding. At its core, welding is about creating connections that don't just. This instructables details how to MIG weld a box made out of old scrap metal. I used 1/8" steel from a local scrap yard. The amount depends on the size of box you want. Plasma cutter or other tool to cut the metal pieces. Aluminum MIG and TIG Reliable, high quality aluminum MIG and TIG welding products with tight tolerances in chemical composition.
[PDF Version]
-
Welding of electrical distribution boxes and cabinets
Understand key welding methods, materials, design and quality-control for electrical enclosures — from TIG/MIG to distortion control and standards compliance. Electrical enclosure welding means joining metal parts like panels and frames to build a strong box that protects electrical equipment.
-
Are ODN products used in 5G
Accordingly, this paper overviews 5G networks along with their requirements and provides a brief summary of OTNs and the corresponding optimization mechanisms. Additionally, this work discusses th.
-

How to weld ceramic ferrules
The stud is inserted into the chuck and - if necessary - equipped with a ceramic ferrule. A lift mechanism in the welding gun or welding head lifts the stud. A secondary arc (pilot arc) of low current is ignited between stud tip and work. Ceramic ferrules are used in stud welding as heat-resistant arc shields that contain molten metal, focus the arc energy, and protect the weld pool from atmospheric contamination during the drawn arc process. Learn more about ceramic ferrules and why they're so important in this blog. The process “Drawn arc stud welding” is used for studs of an approximate diameter of 3 to 25 mm, welding. Arc stud welding (ARC) with ceramic ferrule: The process drawn arc stud welding is mostly used for stud diameters of 3 to 25 mm and a welding time of 100 to 1 500 ms.
[PDF Version]